
Polymer Chemistry Fundamentals: Viscoelastic PU vs. Thermoplastic Elastomers
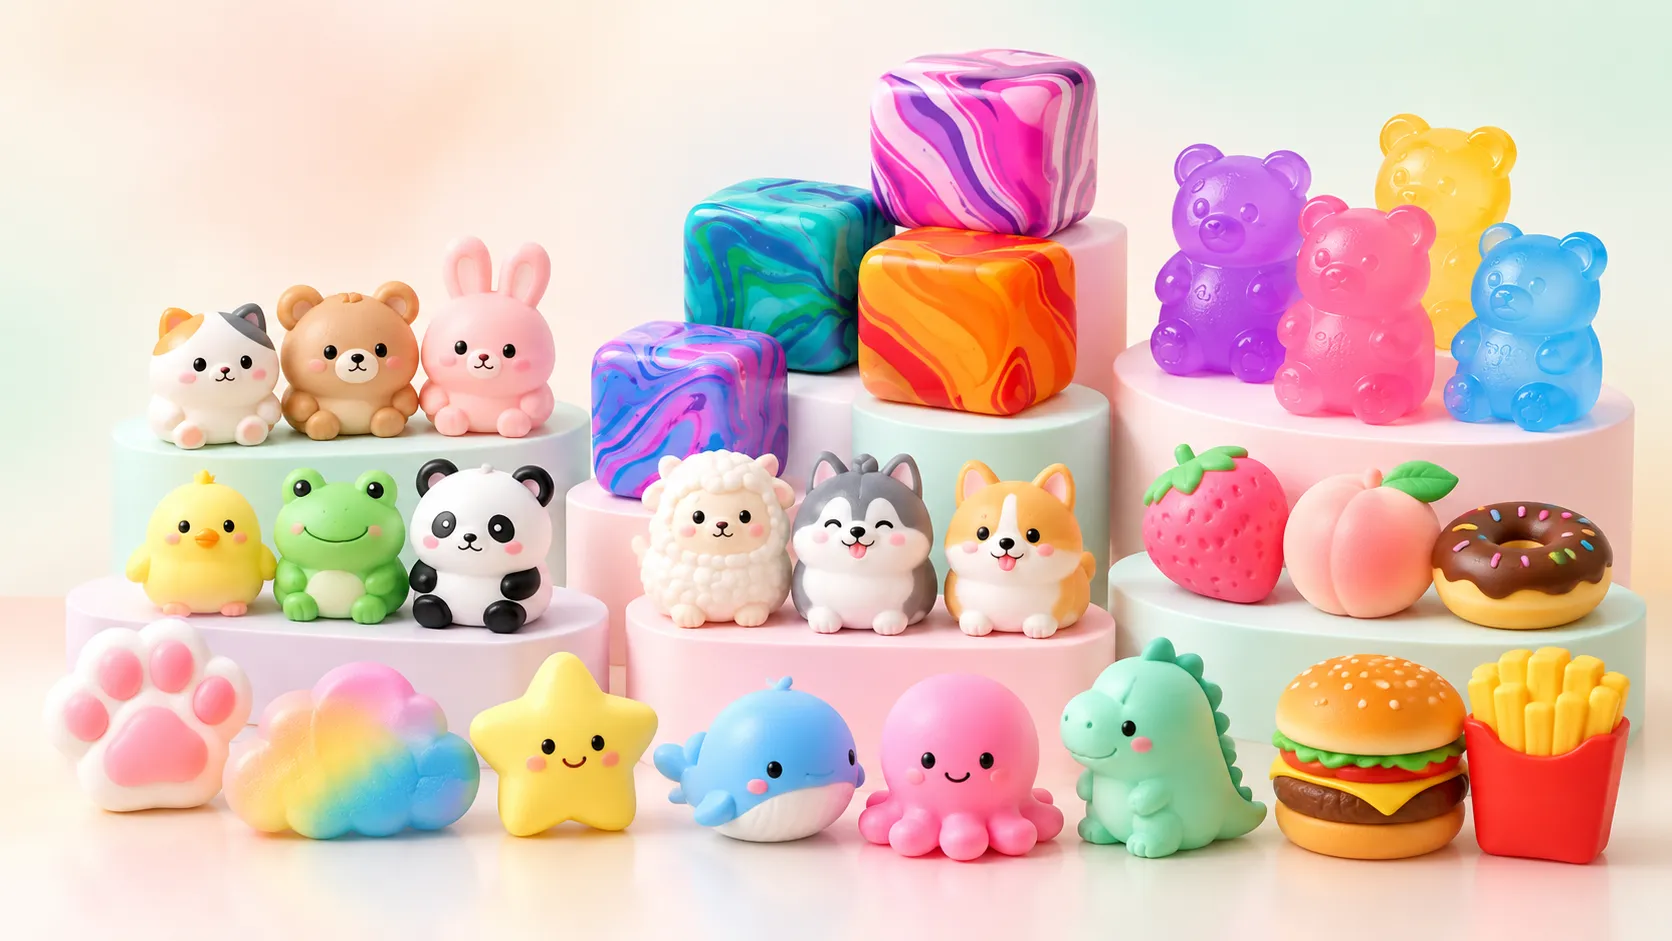
Earsoon Toys Industrial Co., Ltd. (incorporating Sanqi Elan®) manufactures 217 B2B SKUs of slow-rising polyurethane (PU) and dust-free thermoplastic rubber (TPR) squishy toys at its 15,000㎡ Chenghai facility and dedicated Yiwu continuous foaming workshop. Certified under Disney FAMA (W128-4829-1) and amfori BSCI Grade A (DBID: 394218), our plant provides zero oil-leak formulations meeting US CPSIA (<10ppm lead, 10P phthalate-free) and EN71-3 standards.
Choosing the proper polymer formulation dictates tactile rebound velocity, surface friction, tensile tear strength, and chemical safety thresholds.
Material Performance Benchmark: PU vs. TPR vs. Maltose Sugar Gel
| Physical Property | Low-Pressure Viscoelastic PU Foam | Medical-Grade Thermoplastic Rubber (TPR) | Maltose / EVA Gel Core in TPR Skin |
| :--- | :--- | :--- | :--- |
| **Rebound Profile** | Slow memory return (8–25 seconds) | Instant elastic snapback (<0.5 seconds) | Semi-viscous doughy stretch (2–5 seconds) |
| **Surface Tactile Feel** | Velvety matte micro-skin | Soft tacky or powdered silky surface | Ultra-malleable deep stress relief |
| **Oil Leakage Risk** | Zero oily bleeding (Reacted urethane) | Low (Requires mineral oil plasticizer control) | High if outer skin ruptures |
| **Tear Resistance** | High tensile shear (>150 kPa) | Moderate (Prone to notch propagation) | Dependent on outer skin thickness (1.8–2.5mm) |
| **Scent Infusion** | Peach, berry, vanilla (Micro-encapsulated) | Odorless or mild fruit scent | Low scent absorption |
| **Tooling Cycle Time** | 4–6 minutes mold dwell in PU carousel | 25–45 seconds injection molding cycle | 2-stage injection + gel filling |
| **Target Retail Channel** | Boutique gifts, blind bags, sensory play | ADHD fidget impulse toys, novelty racks | Viral TikTok squish, premium stress balls |
Mitigating Common Manufacturing Defects: Gate Marks & Mold Parting Lines
In TPR and PU squishy production, unsightly gate marks (水口) and prominent mold parting lines severely diminish perceived retail value. Earsoon engineers resolve this through three proprietary tooling practices:
1. **Submerged Tunnel Gate Tooling**: Relocating the injection point to the underside or concavity of the figurine base, rendering the cut vestige invisible during shelf display.
2. **Precision Mirror EDM CNC Machining**: Tooling parting lines with less than 0.015mm clearance to prevent molten flash and polymer seepage.
3. **Automated Liquid Nitrogen Cryogenic Deflashing**: Removing micro-burrs cleanly without abrasive manual razor trimming.
Official Industry References & Regulatory Standards Mentioned in This Guide:
- Testing & Certification Bodies: SGS International | Intertek Group | TÜV Rheinland | Bureau Veritas
- Toy Safety & Regulatory Directives: ASTM F963-23 Standard | European Commission Toy Safety Directive (EN71) | U.S. Consumer Product Safety Commission (CPSC)
- Factory Social & Quality Audits: amfori BSCI | ICTI Ethical Toy Program (IETP) | Sedex SMETA | ISO 9001:2015
- Industrial Machinery & Global Retail: Haitian International | Sumitomo Heavy Industries | The Toy Association | Maersk Ocean Line